Sludge mixing plays an important role in wastewater treatment. It helps maintain consistent solids concentration and supports reliable downstream processing.
However, not every sludge stream needs the same mixing method. Thin biological sludge behaves differently from thickened sludge, chemical sludge, or dewatered cake. Choosing the wrong mixer can increase energy consumption, create dead zones, and accelerate equipment wear.
This guide explains the main types of sludge mixing equipment, their applications, and the design factors that influence performance. It also covers mixer selection, maintenance, and integration with other sludge treatment equipment.
Sludge management does not end after mixing. Storage, dewatering, transport, and final biosolids management must work together. The U.S. Environmental Protection Agency’s biosolids resources provide additional information on biosolids management and related regulatory considerations.
Quick Reference: Sludge Mixing Equipment
- Main purpose: Blend sludge, maintain uniformity, and reduce solids separation.
- Common equipment: Tank agitators, submersible mixers, inline mixers, and recirculation systems.
- Typical applications: Sludge storage, thickening, conditioning, and feed preparation.
- Main selection factors: Solids concentration, viscosity, tank geometry, and mixing duty.
- Low-solids sludge: Often suits conventional mechanical or submersible mixing.
- High-solids sludge: May require higher-torque equipment or specialized mixing arrangements.
- Chemical conditioning: Inline mixers can provide rapid blending of chemicals and sludge.
- Key design risk: Excessive mixing can waste energy or damage sensitive flocs.
- Maintenance priorities: Inspect seals, bearings, impellers, drives, and electrical protection.
- Design principle: Match the mixer to the actual sludge properties, not just the tank volume.
1. What Does Sludge Mixing Equipment Do?
Sludge mixing equipment combines sludge, water, chemicals, or different sludge streams to achieve a more uniform mixture. Depending on the process, mixing may also prevent settling and improve the consistency of downstream feed.
Without adequate mixing, solids can accumulate at the bottom of a tank. Meanwhile, lighter material may float or form a surface layer. These conditions create uneven solids concentration and make pumping less predictable.
1.1 Common Reasons for Mixing Sludge
| Application | Mixing objective | Typical equipment |
|---|---|---|
| Sludge storage | Reduce settling and concentration differences | Tank agitator or submersible mixer |
| Sludge blending | Combine different sludge streams | Mechanical mixer or recirculation system |
| Polymer conditioning | Distribute polymer solution through sludge | Inline mixer or controlled tank mixing |
| Lime stabilization | Blend lime with sludge | High-torque mixer or specialized blending system |
| Thickened sludge handling | Maintain a consistent feed | Low-speed agitator or recirculation system |
| Digester operation | Support uniform contents and process stability | Digester mixing system |
| Dewatering feed preparation | Reduce feed variation | Tank agitator or inline mixer |
The required mixing intensity depends on the process. For example, blending polymer into sludge requires a different approach from keeping sludge suspended during storage.
1.2 Mixing Is Not the Same as Pumping
A pump moves sludge from one location to another. In contrast, a mixer creates motion within a tank or pipeline to blend the material.
Some systems use pump recirculation to perform both functions. However, recirculation alone may not eliminate dead zones in a large or poorly shaped tank.
Engineers should therefore assess circulation patterns, solids concentration, and sludge properties before selecting equipment.
2. Main Types of Sludge Mixing Equipment
Different mixer designs suit different sludge characteristics and process requirements. The following options cover common industrial and municipal applications.
2.1 Top-Entry Tank Agitators
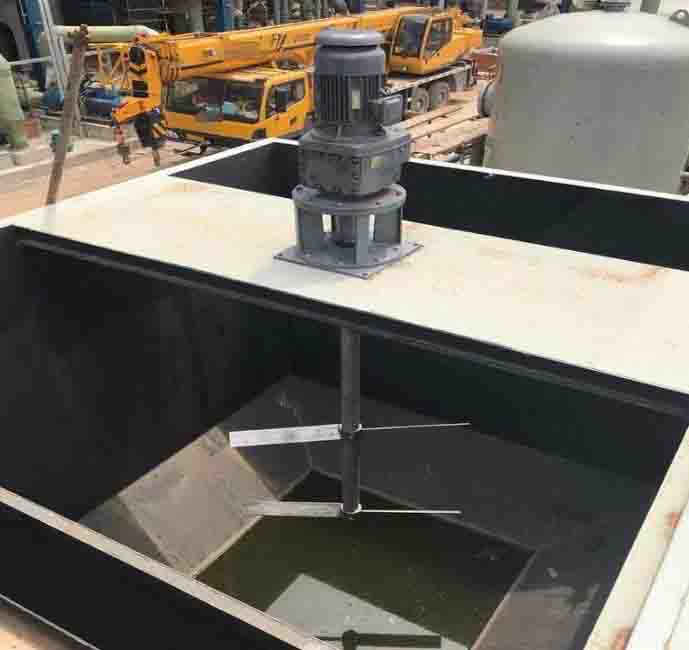
A top-entry agitator mounts above the tank and drives an impeller through a shaft. Depending on the design, the impeller creates axial or radial flow.
These mixers suit many sludge blending and storage applications. They also allow engineers to select different impeller geometries for specific duties.
Nevertheless, shaft alignment, tank access, and mechanical sealing require attention. Thick sludge may also demand greater starting torque than a standard agitator can provide.
2.2 Submersible Sludge Mixers
Submersible mixers operate directly inside the tank. Their compact installation reduces the need for long external shafts and can simplify equipment layout.
They are useful in wastewater tanks, equalization basins, and selected sludge storage applications. However, engineers must verify solids compatibility, immersion requirements, cable protection, and maintenance access.
2.3 Inline Static Mixers
An inline static mixer uses fixed mixing elements inside a pipe. Flow through these elements creates repeated splitting and recombination without a separate rotating drive.
This design can blend polymer solution, chemicals, or compatible sludge streams in a pipeline. It also avoids submerged mechanical components.
On the other hand, static mixers create pressure loss. Highly viscous sludge or pipelines with limited available pressure may therefore require careful hydraulic evaluation.
2.4 Inline Dynamic Mixers
Dynamic inline mixers use a motor-driven rotor or another powered mixing mechanism. They can deliver intensive blending in a compact footprint.
These units may suit applications that need rapid, controlled mixing. However, they introduce moving components, electrical demand, and additional maintenance requirements.
2.5 Pump Recirculation Systems
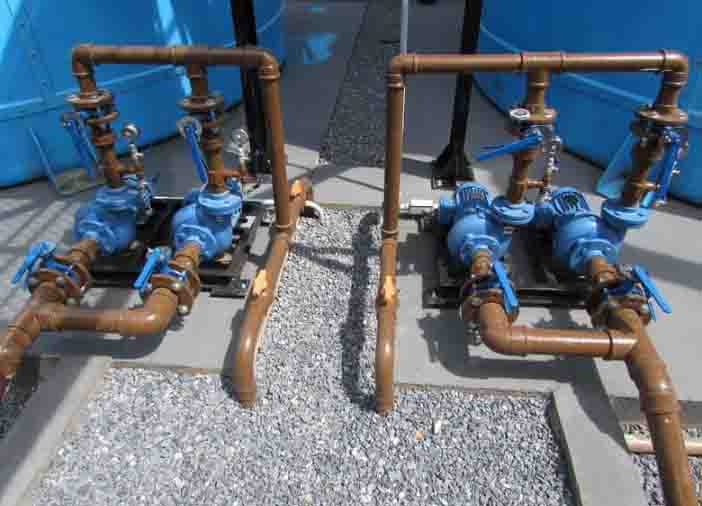
A recirculation system withdraws sludge from a tank and returns it through a discharge line or nozzle. The return flow creates circulation and can help reduce concentration differences.
This arrangement may be practical when the plant already has suitable pumps and piping. Still, nozzle placement and tank geometry strongly influence performance.
A poorly designed return line can circulate sludge near the outlet while leaving stagnant zones elsewhere.
2.6 Mixing Equipment Comparison
| Equipment type | Main advantages | Main limitations | Typical application |
|---|---|---|---|
| Top-entry agitator | Flexible impeller options; accessible drive | Requires shaft support and maintenance access | Storage and blending tanks |
| Submersible mixer | Compact installation; no long external shaft | Requires lifting access and suitable submersible construction | Basins and sludge tanks |
| Static inline mixer | No rotating drive; compact footprint | Pressure loss; limited flexibility after installation | Chemical and polymer blending |
| Dynamic inline mixer | Intensive, controlled blending | Higher mechanical complexity | Specialized conditioning duties |
| Pump recirculation | Can use existing pumping infrastructure | May leave dead zones; consumes pumping energy | Tank circulation and blending |
| High-torque mixer | Suitable for demanding, viscous duties when properly designed | Higher equipment cost and drive requirements | Thick or difficult-to-mix sludge |
No single design is best for every sludge stream. Selection should start with the required process result and verified sludge properties.
3. Key Factors in Sludge Mixer Selection
3.1 Solids Concentration and Viscosity
Sludge concentration affects how the material flows and how much torque the mixer needs. As solids concentration increases, viscosity may rise sharply, depending on sludge composition.
Consequently, a mixer suitable for dilute biological sludge may perform poorly with thickened sludge. Engineers should obtain representative operating data before finalizing the drive and impeller design.
At minimum, confirm:
- Total solids concentration and its normal operating range.
- Sludge density and viscosity, where available.
- Presence of fibers, grit, grease, or other troublesome materials.
- Temperature and any relevant chemical characteristics.
- Whether the sludge tends to settle, float, or form lumps.
3.2 Tank Geometry and Liquid Level
Tank diameter, depth, bottom shape, and internal obstructions affect circulation. A large motor cannot compensate for every problem caused by poor geometry.
For instance, a mixer positioned too high may leave solids near the tank floor. Similarly, an unsuitable impeller direction can create circular flow without enough vertical movement.
Engineers should review the tank drawing, inlet and outlet positions, baffles, and operating liquid levels. Variable liquid levels deserve special attention because the impeller may operate under different conditions.
3.3 Mixing Duty and Intensity
Different applications require different mixing results. Storage may need continuous or intermittent circulation, while chemical conditioning may require rapid blending over a short contact time.
Excessive mixing can waste power and may disrupt flocs formed during chemical conditioning. Therefore, the design should define the desired outcome instead of simply maximizing mixer speed.
| Mixing duty | Main objective | Design consideration |
|---|---|---|
| Storage | Limit settling and stratification | Tank coverage and operating schedule |
| Blending | Achieve a uniform mixture | Flow pattern and residence time |
| Polymer addition | Distribute polymer without excessive shear | Injection point and mixing intensity |
| Lime stabilization | Blend solids and chemical thoroughly | Torque, abrasion, and process requirements |
| Thickened sludge holding | Maintain consistent feed properties | Viscosity and restart conditions |
3.4 Continuous or Intermittent Operation
Continuous mixing can maintain a more uniform tank condition, but it also increases energy use and operating hours. Intermittent operation may reduce energy demand when the sludge settles slowly enough.
However, a timer-based schedule should not replace performance checks. If solids settle rapidly during idle periods, the mixer may struggle to restart or restore uniformity.
A practical commissioning plan should test different operating intervals and monitor solids distribution, motor load, and pump performance.
3.5 Materials and Corrosion Resistance
Sludge composition varies between municipal and industrial facilities. Chemical sludge may contain corrosive compounds, while grit and mineral solids can cause abrasive wear.
For this reason, engineers should confirm the compatibility of wetted materials, seals, fasteners, and protective coatings. Stainless steel may suit some duties, but the correct grade depends on the actual chemical environment.
A material upgrade alone will not solve problems caused by poor impeller design or excessive abrasion.
4. Basic Sizing and Design Considerations
Mixer sizing requires more than matching motor power to tank volume. The engineer must consider tank geometry, sludge properties, required circulation, and the process result.
4.1 Calculate the Working Volume
For a rectangular tank:
Working Volume (m³) = Tank Length (m) × Tank Width (m) × Working Liquid Depth (m)
For a cylindrical tank:
Working Volume (m³) = π × Tank Radius² (m²) × Working Liquid Depth (m)
Use the actual working liquid level rather than the full structural tank height. Freeboard, dead volume, and minimum operating level may reduce the usable volume.
4.2 Review the Required Mixing Duty
A preliminary review should establish the operating duty before equipment selection. The following parameters provide a practical starting point.
| Parameter | Information required | Why it matters |
|---|---|---|
| Tank working volume | Usable volume in m³ | Defines the mixing space |
| Sludge concentration | Total solids, % | Influences viscosity and torque |
| Sludge properties | Density, viscosity, fiber and grit content | Affects mixer and material selection |
| Mixing objective | Suspension, blending, or conditioning | Defines the required result |
| Operating schedule | Continuous or intermittent | Influences motor duty and energy use |
| Tank dimensions | Diameter, depth, bottom profile | Determines circulation pattern |
| Chemical exposure | pH and relevant compounds | Guides material selection |
| Installation conditions | Indoor, outdoor, submerged, or enclosed | Affects protection and maintenance access |
4.3 Estimate Energy Demand Carefully
Motor power depends on the mixer design, impeller geometry, speed, and sludge resistance. Tank volume alone does not provide a reliable motor rating.
Therefore, avoid selecting a motor from a generic power-per-cubic-meter figure without checking the application. Request the manufacturer’s sizing basis and operating limits for the specified sludge conditions.
Where the sludge properties vary significantly, include the expected minimum and maximum concentrations in the equipment inquiry.
4.4 Confirm Hydraulic and Mechanical Compatibility
The mixer must work with the tank, pipework, and downstream equipment. Check nozzle clearances, pipe velocities, pressure losses, and available pump head where applicable.
For inline systems, also verify the available straight pipe length and the pressure drop across the mixing element. These details can affect both installation cost and operating performance.
5. Integration with Sludge Treatment Equipment
Mixing is usually one part of a larger sludge handling process. Its design should reflect what happens immediately before and after the mixing stage.
5.1 Integration with Sludge Thickening
Thickening increases solids concentration and reduces the volume requiring further treatment. However, thickened sludge often has different flow behavior from dilute sludge.
A mixer installed after thickening should therefore suit the higher solids concentration. Review the outlet arrangement and transfer pump together to avoid uneven feed or unnecessary recirculation.
See the related guide on sludge thickening equipment for more information about solids concentration and volume reduction.
5.2 Integration with Sludge Dewatering
Dewatering equipment performs best when feed conditions remain within its intended operating range. Uneven solids concentration can affect throughput, polymer demand, and cake consistency.
A properly designed mixing tank can help stabilize feed conditions. However, mixing cannot compensate for incorrect polymer dosage, unsuitable sludge chemistry, or inadequate dewatering capacity.
Review the complete feed preparation system before changing mixer speed or motor power. See the related guide on sludge dewatering equipment for more information.
5.3 Integration with Storage and Conveying
Storage tanks may need mixing to reduce settling during holding periods. Once sludge leaves the tank, pumps, conveyors, and pipelines must handle the resulting material consistently.
For this reason, confirm the transfer method and downstream equipment before finalizing the mixer. A design that works well in the tank may still create difficulties if the outlet contains settled solids or the transfer system cannot handle the sludge.
Related reading: sludge storage systems and sludge conveying equipment.
6. Installation and Maintenance
Reliable performance depends on correct installation and a maintenance plan that reflects the operating environment. Routine checks can identify problems before they interrupt the treatment process.
6.1 Installation Checklist
- Confirm the tank dimensions and mixer mounting arrangement.
- Check impeller clearance from walls, floors, and internal structures.
- Verify motor voltage, frequency, protection rating, and control requirements.
- Confirm that lifting or removal access is available.
- Inspect seals, fasteners, couplings, and electrical connections.
- Verify that the mixer suits the minimum and maximum operating liquid levels.
- Test rotation direction and operating current during commissioning.
- Record baseline vibration, noise, and motor load.
6.2 Maintenance Schedule
| Frequency | Component | Inspection or task |
|---|---|---|
| Daily | Mixer and tank | Check for unusual noise, vibration, or visible settling |
| Weekly | Motor and controls | Review operating status, alarms, and current readings |
| Monthly | Impeller and shaft | Inspect for wear, buildup, and loose fasteners |
| Monthly | Seals and connections | Check for leakage or damage where accessible |
| Quarterly | Electrical system | Inspect connections and protective devices according to site procedures |
| Quarterly | Tank and mounting | Check corrosion, mounting integrity, and access equipment |
| Annually | Complete assembly | Conduct a planned inspection based on manufacturer guidance |
Actual intervals should follow the manufacturer’s instructions and the site’s maintenance requirements. Abrasive or corrosive sludge may require more frequent inspections.
6.3 Common Problems and Troubleshooting
| Symptom | Possible cause | Recommended action |
|---|---|---|
| Solids accumulate at the tank bottom | Poor circulation or unsuitable impeller position | Review mixer placement and circulation pattern |
| Motor overloads | High viscosity, obstruction, or mechanical fault | Check sludge properties, impeller condition, and motor load |
| Excessive vibration | Misalignment, damaged impeller, or loose mounting | Inspect the assembly and correct the mechanical issue |
| Uneven chemical blending | Incorrect injection point or inadequate mixing | Review dosing location and mixing duty |
| Frequent seal failures | Abrasive sludge, chemical incompatibility, or poor installation | Check materials, operating conditions, and installation |
| Mixer fails to restart | Settled solids, excessive starting load, or electrical fault | Check tank condition and follow safe troubleshooting procedures |
| High energy consumption | Excessive speed or unnecessary operating hours | Review the mixing objective and operating schedule |
Do not increase motor power automatically when performance declines. First determine whether the cause is sludge variability, poor circulation, mechanical wear, or incorrect operation.
7. Illustrative Project Scenarios
The following scenarios are illustrative engineering examples, not verified customer projects. They show how application requirements can influence equipment selection.
Scenario A: Municipal Sludge Storage
- Region: Southeast Asia
- Scale: Municipal wastewater treatment plant
- Problem: Solids accumulated near the bottom of a sludge holding tank.
- Approach: Review mixer placement, tank geometry, and the operating schedule.
- Expected outcome: More consistent sludge conditions and fewer transfer interruptions, subject to commissioning verification.
Scenario B: Industrial Sludge Conditioning
- Region: Central Europe
- Scale: Industrial wastewater treatment facility
- Problem: Chemical addition produced inconsistent sludge conditioning.
- Approach: Assess the injection point, inline mixing requirements, and sludge characteristics.
- Expected outcome: Improved chemical distribution when the selected mixer matches the actual process conditions.
Scenario C: Thickened Sludge Transfer
- Region: North America
- Scale: Large wastewater treatment facility
- Problem: Thickened sludge caused variable feed conditions before dewatering.
- Approach: Evaluate solids concentration, mixer torque, tank circulation, and transfer pump compatibility.
- Expected outcome: More stable feed preparation, subject to operating tests and equipment verification.
8. Common Sludge Mixer Selection Mistakes
Mistake 1: Selecting by Tank Volume Alone
Two tanks with the same volume can contain sludge with very different mixing requirements. Solids concentration, viscosity, and tank geometry all influence performance.
Instead, provide the supplier with actual operating data and define the required mixing result.
Mistake 2: Assuming More Power Always Means Better Mixing
Higher motor power may increase energy consumption without resolving dead zones or poor impeller placement. In some conditioning processes, excessive shear can also harm the desired floc structure.
Consequently, mixer geometry and flow patterns deserve as much attention as motor rating.
Mistake 3: Ignoring Restart Conditions
Sludge may settle during a shutdown. A mixer that operates normally in a uniform tank may struggle to restart after solids accumulate.
Discuss the expected shutdown duration, settling behavior, and restart requirements before finalizing the design.
Mistake 4: Treating Mixing and Chemical Conditioning as the Same Duty
General tank circulation and rapid chemical blending require different mixing conditions. A system optimized for storage may not provide the appropriate conditions for polymer addition.
Define each process duty separately, especially when one tank serves multiple functions.
Mistake 5: Overlooking Maintenance Access
A mixer may fit the tank drawing but remain difficult to remove or service after installation. This can increase downtime and maintenance cost.
Check lifting arrangements, headroom, isolation procedures, and access for routine inspections during the design stage.
9. Information to Include in a Mixer RFQ
A detailed request for quotation helps suppliers recommend equipment that suits the actual application.
| RFQ item | Information to provide |
|---|---|
| Application | Storage, blending, conditioning, or other duty |
| Tank dimensions | Length, width, depth, diameter, and bottom shape |
| Working volume | Normal, minimum, and maximum liquid levels |
| Sludge data | Solids concentration, density, viscosity, and temperature |
| Sludge composition | Fibers, grit, grease, chemicals, and corrosive compounds |
| Mixing requirements | Suspension, uniformity, or chemical blending objective |
| Operating mode | Continuous, intermittent, and expected shutdown periods |
| Installation | Top-entry, submersible, inline, or recirculation |
| Electrical supply | Voltage, frequency, phase, and control requirements |
| Materials | Required wetted materials and corrosion considerations |
| Site conditions | Indoor or outdoor use, ambient conditions, and access limitations |
| Documentation | General arrangement drawing, datasheet, manual, and maintenance requirements |
If some data remain unavailable, identify the assumptions clearly. The supplier can then state which parameters require confirmation before final sizing.
10. Engineering Recommendation
The best sludge mixer is not necessarily the largest or most powerful unit. It is the equipment that achieves the required mixing result under the actual operating conditions.
For dilute sludge, a conventional agitator or submersible mixer may provide a practical solution. Meanwhile, thickened sludge often requires closer evaluation of viscosity, starting torque, and circulation patterns. Inline mixers suit selected chemical blending duties, provided that pressure loss remains acceptable.
Before purchasing, confirm the sludge characteristics, tank geometry, mixing objective, and downstream transfer requirements. Also review maintenance access and expected operating hours. These checks help avoid equipment mismatches that become expensive after installation.
Frequently Asked Questions
1. What is sludge mixing equipment used for?
Sludge mixing equipment blends sludge streams, maintains more uniform solids concentration, and helps reduce settling in selected applications. It can also support chemical conditioning and downstream treatment. The required mixing method depends on the sludge properties and process objective.
2. Which mixer is suitable for thickened sludge?
The answer depends on solids concentration, viscosity, tank geometry, and restart requirements. A high-torque agitator or specialized mixing arrangement may suit demanding applications. However, engineers should verify the actual sludge properties before choosing a model.
3. Does every sludge storage tank need a mixer?
No. Some tanks can operate without continuous mixing, depending on sludge behavior and storage duration. Nevertheless, rapid settling or concentration variation may justify mechanical mixing or recirculation. A site-specific assessment should determine the appropriate arrangement.
4. Can a static mixer blend sludge and polymer?
Yes, a static mixer can blend polymer solution with compatible sludge streams in a pipeline. Its performance depends on flow rate, viscosity, injection arrangement, and pressure loss. Excessive shear or poor chemical preparation can still affect conditioning results.
5. How should a sludge mixer be maintained?
Follow the manufacturer’s maintenance instructions and the site’s safety procedures. Inspect the impeller, shaft, seals, mounting, motor load, and electrical protection at suitable intervals. In addition, monitor vibration, noise, settling, and changes in operating current to identify emerging problems.
Need Help Selecting Sludge Mixing Equipment?
Morvolous supports wastewater treatment equipment selection for sludge handling and process integration. Share your tank dimensions, sludge concentration, operating conditions, and mixing objectives to help define a suitable configuration.
A clear equipment specification can reduce selection uncertainty and improve coordination between mixing, storage, pumping, and dewatering stages.
Contact the Morvolous team to discuss your sludge mixing application and equipment requirements.
Author: Morvolous Engineering Team
Morvolous provides engineering-oriented information on wastewater treatment equipment, sludge handling, and system selection. Final equipment specifications should be confirmed against actual process data and site conditions.