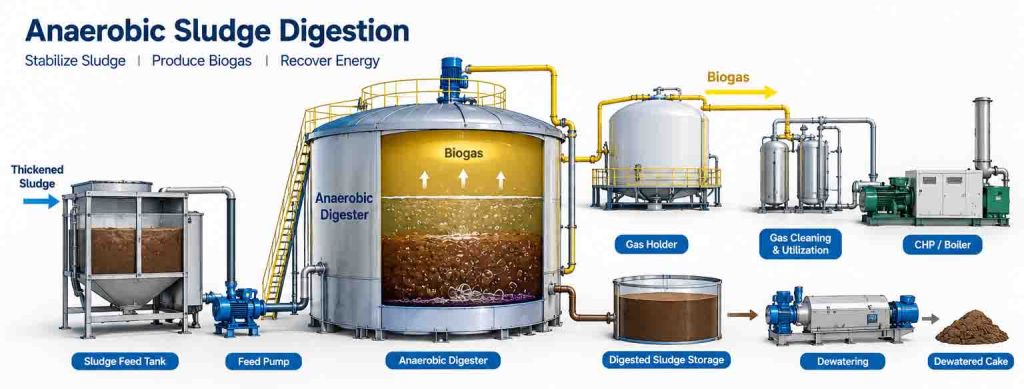
Anaerobic sludge digestion is an important process in large wastewater treatment plants. It stabilizes organic solids without oxygen and produces biogas as a useful by-product.
The process can reduce sludge quantity, odors, and biodegradable organic matter. It can also create an energy source when the generated biogas is properly collected and used.
For many wastewater plants, digestion sits between sludge thickening and final dewatering. The exact arrangement depends on sludge characteristics, treatment objectives, available space, and energy requirements.
The U.S. EPA identifies wastewater solids as one of the major feedstocks for anaerobic digestion. Its technical resources also cover digester types, operating temperatures, biogas use, and biosolids management. For additional engineering reference, see the EPA’s anaerobic digestion and biosolids resources.
Quick Reference: Anaerobic Sludge Digestion
| Parameter | Typical Reference / Design Consideration |
|---|---|
| Process condition | Oxygen-free biological treatment |
| Common mesophilic range | About 30–38°C |
| Common mesophilic design temperature | About 35°C |
| Typical thermophilic range | About 50–60°C |
| Mesophilic single-stage SRT | Often around 20 days |
| Multi-stage SRT example | Often around 14–18 days |
| Common digester feed | Thickened primary and/or secondary sludge |
| Main gas products | Methane and carbon dioxide |
| Main energy product | Biogas |
| Typical methane fraction | Often around 60–70% of biogas |
| Main biological target | Volatile organic solids |
| Main outputs | Biogas + stabilized digestate |
| Main equipment | Digester tank, mixer, heater, gas system, pumps |
| Downstream process | Thickening, dewatering, storage, or further treatment |
These figures are preliminary references rather than universal design values. Actual performance depends on sludge composition, temperature, loading, retention time, mixing, and process configuration. EPA references commonly describe mesophilic digestion around 35°C and thermophilic operation around 50–60°C.
What Is Anaerobic Sludge Digestion?
Anaerobic digestion is a biological process that occurs without oxygen.
Microorganisms break down biodegradable organic matter through several biological stages. Methane-forming microorganisms eventually convert intermediate products into methane and carbon dioxide.
The resulting gas is called biogas.
A simplified process is:
Thickened Sludge → Anaerobic Digester → Biogas + Stabilized Sludge
The digested sludge then continues to dewatering or another downstream treatment process.
The EPA describes anaerobic digestion as a process that stabilizes wastewater solids, reduces odors and pathogens, and converts part of the volatile solids fraction into biogas.
Why Digest Wastewater Sludge?
Raw sludge contains biodegradable organic matter. If it is stored without adequate stabilization, biological activity can continue.
This can cause:
- Odor generation
- Gas formation
- Increased biological activity
- Poor storage stability
- Higher disposal challenges
Digestion reduces the biodegradable fraction before final handling.
The process also changes the physical and chemical characteristics of the sludge. These changes can affect downstream dewatering performance.
Sludge Stabilization
Stabilization is one of the main reasons to install a digester.
The microorganisms consume part of the biodegradable organic material. The remaining solids become more stable.
This can reduce the potential for odor and biological activity during later storage or handling.
Biogas Production
Biogas is another major benefit.
The gas mainly contains methane and carbon dioxide. Methane provides the useful energy component.
Captured biogas can be used for heating, electricity generation, or other energy recovery applications. The EPA notes that wastewater resource recovery facilities use digester gas for electricity and useful heat in many installations.
Reduction of Solids
Anaerobic treatment converts part of the volatile solids into gas.
The actual reduction depends on the biodegradable fraction of the sludge. Primary sludge, waste activated sludge, and co-digested materials can produce different results.
Where Does the Digester Fit in a Sludge Treatment Line?
A common sludge treatment sequence is:
Primary Sludge + Waste Activated Sludge
↓
Sludge Thickening
↓
Anaerobic Digestion
↓
Digested Sludge Storage
↓
Polymer Conditioning
↓
Sludge Dewatering
↓
Dewatered Cake
The biogas leaves the digester through a separate gas collection system.
This arrangement explains why sludge thickening is important before digestion. Lower water content means more organic solids can be processed within the available digester volume.
It also connects directly with the previous article on sludge thickening. A thickener can reduce hydraulic loading before the digestion stage.
How Anaerobic Digestion Works
Anaerobic digestion is not one single biological reaction.
Several groups of microorganisms participate in the process.
The main stages are commonly described as:
Hydrolysis → Acidogenesis → Acetogenesis → Methanogenesis
Hydrolysis
Large organic molecules are broken into smaller soluble compounds.
Proteins, carbohydrates, and fats are converted into simpler materials.
This stage makes the organic matter more accessible to subsequent microorganisms.
Acidogenesis
Acid-forming bacteria convert soluble compounds into organic acids and other intermediates.
Volatile fatty acids become important process indicators at this stage.
Acetogenesis
Intermediate compounds are converted into acetate, hydrogen, and carbon dioxide.
These products become substrates for methane-forming microorganisms.
Methanogenesis
Methanogenic microorganisms convert acetate and hydrogen-based compounds into methane.
This stage is sensitive to process conditions.
The methane-forming population generally requires stable temperature, pH, loading, and mixing.
The EPA describes these biological stages and notes that acid-forming organisms respond differently to environmental changes than methanogenic organisms.
Mesophilic vs Thermophilic Digestion
Temperature is one of the most important design variables.
Two major operating ranges are widely used:
- Mesophilic: approximately 30–38°C
- Thermophilic: approximately 50–60°C
Many wastewater digesters operate under mesophilic conditions because the process is comparatively stable and easier to operate.
Thermophilic digestion can provide faster biological reactions and stronger pathogen reduction. However, it normally requires more heating energy and tighter process control.
EPA technical references describe mesophilic digestion around 30–38°C and thermophilic systems around 50–60°C.
Mesophilic Digestion
A common design temperature is around 35°C.
The system needs continuous or controlled heating to maintain a stable biological environment.
Mesophilic digestion is widely used because it provides a practical balance between process stability and energy demand.
Thermophilic Digestion
Thermophilic systems operate at substantially higher temperatures.
The faster reaction rate can reduce required retention time in some designs. Pathogen reduction can also improve.
The higher temperature creates additional operating requirements. Heating demand and process sensitivity should therefore be included in the economic evaluation.
Single-Stage vs Multi-Stage Digestion
Digesters can be arranged as one stage or multiple stages.
A single-stage system performs the biological reactions in one main vessel.
A multi-stage system separates different biological environments.
One common arrangement is:
Acid-Phase Digester → Methane-Phase Digester
The first stage promotes hydrolysis and acid formation. The second stage provides conditions for methanogenesis.
The separation can improve process control.
EPA technical information describes multi-stage systems that physically separate acid-forming and gas-forming stages. Some facilities also use thermophilic and mesophilic stages in sequence.
When Is Multi-Stage Digestion Useful?
Multi-stage systems become more attractive when process control is important.
They can also support different temperature conditions between stages.
However, additional tanks and equipment increase capital cost.
The final choice should consider plant scale and operating objectives.
Wet vs Dry Anaerobic Digestion
Anaerobic digesters can also be classified by feed solids concentration.
Wet or low-solids systems generally handle pumpable slurries below about 15% solids.
Dry or high-solids systems operate with much higher solids concentrations and can handle stackable feedstocks.
For wastewater sludge treatment, wet digestion is common because the feed remains pumpable.
The EPA uses 15% solids as a general distinction between wet and dry anaerobic digestion systems.
Main Anaerobic Digester Equipment
A digester is more than a tank.
A complete system normally includes several mechanical and process components.
Digester Tank
The tank provides the required volume for biological treatment.
Tank geometry depends on the required capacity, retention time, operating pressure, mixing method, and heating arrangement.
Concrete and steel designs are both used in wastewater applications.
Sludge Feed Pump
The feed pump transfers thickened sludge into the digester.
Pump selection should consider:
- Solids concentration
- Flow rate
- Pressure
- Particle size
- Abrasive content
- Pumping frequency
Positive displacement pumps are often considered for thick sludge because they can provide controlled flow.
Sludge Recirculation Pump
Recirculation can improve heat distribution and mixing.
The pump draws sludge from the digester and returns it through an external circulation loop.
An external heat exchanger can also be installed within this loop.
Digester Mixer
Mixing prevents excessive solids accumulation.
It also distributes heat and helps maintain a more uniform biological environment.
Possible mixing methods include:
- Mechanical mixers
- Gas recirculation
- Sludge recirculation
- Combined systems
The best arrangement depends on tank geometry and sludge characteristics.
Heating System
Digesters need temperature control when operated under mesophilic or thermophilic conditions.
A typical heating system may include:
Boiler / Heat Source → Hot Water Pump → Heat Exchanger → Digester
Recovered engine heat from a combined heat and power system can also be used.
The objective is not simply to add heat. The system must maintain stable temperature across the entire digester volume.
Gas Collection System
Biogas leaves the digester through a controlled gas collection line.
A typical gas system includes:
- Gas piping
- Pressure control
- Moisture removal
- Flame arrestor
- Gas safety devices
- Gas storage
- Flare or utilization equipment
Biogas contains methane, so gas systems require appropriate safety engineering.
Gas Holder
A gas holder buffers variations between gas production and gas consumption.
This allows the plant to continue producing biogas even when the energy recovery system is not consuming gas at the same rate.
Flare
A flare provides controlled combustion when biogas cannot be used.
It can also serve as an emergency or backup disposal route for excess gas.
The final gas management system depends on local regulations and the selected energy recovery system.
Anaerobic Sludge Digestion Equipment Comparison
| Equipment | Main Function | Key Design Concern | Typical Control |
|---|---|---|---|
| Digester tank | Biological treatment | Volume and retention time | Level / temperature |
| Sludge feed pump | Feed control | Solids concentration | Flow / pressure |
| Recirculation pump | Heat and solids circulation | Flow and wear | Flow / pressure |
| Mixer | Maintain uniform sludge | Mixing intensity | Motor load |
| Heat exchanger | Temperature control | Heat transfer | Temperature |
| Boiler / heat source | Generate heat | Fuel or recovered energy | Temperature |
| Gas holder | Gas buffering | Storage volume | Pressure |
| Gas treatment | Protect downstream equipment | Moisture / contaminants | Pressure / alarms |
| Flare | Emergency gas disposal | Safe combustion | Pressure / ignition |
| CHP unit | Energy recovery | Gas quality and flow | Electrical / thermal output |
Key Design Parameter: Solids Retention Time
Solids retention time is one of the most important digestion design parameters.
A longer retention time generally allows more biological stabilization. However, larger retention time requires a larger reactor volume for the same daily solids load.
The design therefore balances:
Digestion Performance vs Reactor Volume vs Capital Cost
EPA technical material reports an example average SRT of about 20 days for mesophilic single-stage systems. Multi-stage systems in the cited literature often use shorter SRT ranges, such as 14–18 days.
These figures should not be copied directly into a project specification. The correct value depends on sludge composition and treatment targets.
Digester Loading
The digester can be evaluated using organic loading.
A common expression is:
OLR = kg VS fed per m³ of digester volume per day
Where:
- OLR = Organic Loading Rate
- VS = Volatile Solids
For example, a digester receiving 1,000 kg VS/day with a working volume of 2,000 m³ has:
OLR = 1,000 ÷ 2,000 = 0.5 kg VS/m³·day
The selected loading rate should match the biological process.
Overloading can increase volatile acids and destabilize methanogenesis.
Underloading may waste available reactor capacity.
Biogas Production
Biogas production depends mainly on the amount and biodegradability of organic material.
The basic relationship is:
Organic Matter → Biogas → Methane + Carbon Dioxide
Methane provides the main energy value.
The actual gas yield varies significantly with feedstock. Primary sludge often behaves differently from waste activated sludge.
Co-digestion can also change gas production.
The EPA notes that wastewater solids, food waste, manure, and fats, oils, and grease can all be used as anaerobic digestion feedstocks.
Biogas Utilization Options
Captured biogas can be used in several ways.
Digester Heating
The simplest use is heating the digester.
This creates a direct relationship between gas production and process energy demand.
Combined Heat and Power
A CHP unit can convert methane into electricity and useful heat.
Electricity can supply plant equipment. Recovered heat can maintain digester temperature.
This arrangement can improve overall energy efficiency.
Boiler Fuel
Biogas can replace part of the conventional boiler fuel.
The gas is burned to generate hot water or steam.
Renewable Natural Gas
With appropriate upgrading, biogas can be processed into a methane-rich fuel.
This requires additional gas purification and upgrading equipment.
The feasibility depends on gas quality, project scale, local regulations, and available infrastructure.
Gas Quality Matters
Raw biogas contains more than methane.
Typical components include:
- Methane
- Carbon dioxide
- Water vapor
- Hydrogen sulfide
- Trace gases
Hydrogen sulfide is especially important because it can cause corrosion.
Moisture can also condense inside gas piping.
Gas conditioning may therefore include:
Moisture Removal → H₂S Reduction → Pressure Regulation → Utilization
The required treatment depends on the selected end use.
Project Anchor: Municipal Sludge Stabilization
Representative project scenario — North America
A municipal facility processed roughly 12,000 m³/day of wastewater. Primary and secondary sludge were combined before digestion.
The plant needed better sludge stabilization and wanted to recover energy from the organic fraction.
The engineering review compared single-stage and multi-stage digestion. A mesophilic system was favored because stable operation was more important than reducing reactor retention time.
The final process included thickening, digestion, biogas collection, and downstream dewatering.
Project Anchor: Limited Energy Recovery
Representative project scenario — Western Europe
A wastewater plant generated roughly 4,000 kg DS/day. Existing sludge handling relied on mechanical dewatering.
The plant considered anaerobic digestion because sludge disposal costs were increasing.
The energy study showed that the gas production could offset part of the digester heating demand. The project therefore prioritized stable gas collection and heat recovery.
The design included a digester, gas holder, flare, and heat recovery system.
Project Anchor: Industrial Organic Sludge
Representative project scenario — Southeast Asia
An industrial facility generated roughly 50 m³/day of organic sludge.
The original sludge management route required frequent off-site disposal.
The engineering team evaluated anaerobic digestion together with sludge thickening. The higher-solids feed reduced the liquid load entering the digester.
The proposed process used controlled feeding, mixing, temperature monitoring, and biogas collection.
The main project objective was stable organic-solids reduction rather than maximum electricity production.
Anaerobic Digestion and Sludge Dewatering
Digestion changes sludge characteristics before final dewatering.
Some digested sludge can dewater differently from raw sludge. Polymer demand may also change.
A complete design should therefore test the digested sludge rather than assume that the same dewatering settings will remain effective.
The downstream process may be:
Digester → Digested Sludge Storage → Polymer Dosing → Screw Press / Centrifuge → Cake
This connects anaerobic digestion directly with the sludge dewatering equipment discussed in the previous articles.
Does Digestion Replace Dewatering?
No.
The two processes have different objectives.
Digestion stabilizes organic solids.
Dewatering removes water.
A treatment plant may use both.
Digestion can reduce the volatile solids fraction. Dewatering then reduces the remaining water content.
The final cake can be transported, stored, disposed of, or further processed according to the project requirements.
Common Anaerobic Digestion Problems
High Volatile Fatty Acids
Rapid acid production can exceed the ability of methane-forming microorganisms to consume the intermediates.
This can destabilize the digester.
Check feed loading, alkalinity, temperature, and mixing before increasing feed rate.
Low Biogas Production
Possible causes include:
- Low organic loading
- Poor sludge biodegradability
- Low temperature
- Insufficient retention time
- Toxic compounds
- Poor mixing
Gas production should be evaluated together with feed solids and VS destruction.
Excessive Foam
Foaming can interfere with gas collection and tank operation.
Possible causes include high organic loading, surfactants, filamentous organisms, or unstable digestion.
Mechanical design should include appropriate foam management.
Uneven Temperature
Poor mixing can create temperature gradients.
The temperature sensor may show a normal value while part of the tank remains outside the desired range.
Mixing and heat distribution should therefore be considered together.
Scum Accumulation
Floating material can accumulate near the surface.
Grease and fibrous material can increase the risk.
The digester should include appropriate scum control and access for maintenance.
Operation and Maintenance
Anaerobic digestion requires more process control than a simple sludge holding tank.
Daily monitoring should include:
- Digester temperature
- Feed flow
- Gas production
- Gas pressure
- pH
- Volatile fatty acids
- Alkalinity
- Sludge level
- Mixer operation
Longer-term monitoring should also include:
- VS reduction
- Gas composition
- Methane concentration
- H₂S
- Dewatering performance
- Polymer consumption
EPA technical resources emphasize process monitoring, equipment operation, temperature control, mixing, gas handling, and sludge characteristics when managing anaerobic digesters.
Safety Considerations
Biogas systems require careful safety engineering.
Methane is flammable. Hydrogen sulfide can also present a serious hazard.
A complete system should consider:
- Gas-tight equipment
- Pressure relief
- Gas detection
- Ventilation
- Flame protection
- Electrical classification
- Emergency shutdown
- Safe flare operation
- Gas piping drainage
The digester building and gas equipment should be designed according to applicable local codes.
Safety requirements should be established during the engineering stage rather than added after installation.
When Is Anaerobic Digestion Worth Considering?
Anaerobic digestion is particularly attractive when a plant has:
- Significant sludge production
- High biodegradable organic content
- Large daily solids loading
- High sludge disposal costs
- A need for stabilization
- Potential for biogas recovery
- Suitable space for digestion equipment
Small facilities may find the capital cost difficult to justify.
In those cases, simpler stabilization and dewatering methods may be more economical.
Engineer’s View: Design the Whole Sludge Line
Anaerobic digestion should not be evaluated as an isolated tank.
The upstream thickening system affects digester loading. Digester performance affects gas production and sludge characteristics. The downstream dewatering system affects the final disposal cost.
The complete chain should therefore be evaluated:
Thickening → Digestion → Gas Recovery → Dewatering → Cake Handling
The best design balances biological performance with equipment cost and operating requirements.
<div class=”opinion-box”>
Engineering position: Do not size a digester from hydraulic flow alone. Dry solids, volatile solids, organic loading, retention time, temperature, and downstream sludge handling should all be considered together.
</div>
Anaerobic Sludge Digestion Selection Checklist
Before selecting a digester system, confirm:
- What is the daily sludge flow?
- What is the feed solids concentration?
- What is the volatile solids concentration?
- What is the daily VS loading?
- Is the feed primary, secondary, or mixed sludge?
- Is thickening required before digestion?
- What temperature range is required?
- What retention time is appropriate?
- Is single-stage digestion sufficient?
- Is multi-stage digestion economically justified?
- What mixing method will be used?
- How will the digester be heated?
- What biogas production is expected?
- How will H₂S and moisture be managed?
- Will biogas be used for heating, CHP, or upgrading?
- How will digested sludge be dewatered?
- What safety systems are required?
FAQ
What is the main purpose of anaerobic sludge digestion?
The main purpose is to stabilize wastewater sludge by biologically converting part of its biodegradable organic matter without oxygen. The process also produces biogas containing methane and carbon dioxide.
What temperature is commonly used for anaerobic sludge digestion?
Mesophilic digestion commonly operates around 30–38°C, with approximately 35°C being a common design condition. Thermophilic systems generally operate around 50–60°C.
Does anaerobic digestion produce biogas?
Yes. Microorganisms convert biodegradable organic matter into biogas. Methane and carbon dioxide are the major components, although the exact gas composition depends on the feedstock and process.
Can digested sludge go directly to a screw press?
It can, provided the feed concentration and sludge characteristics are suitable. In many systems, digested sludge is stored and conditioned with polymer before mechanical dewatering.
Is anaerobic digestion suitable for every wastewater plant?
No. The technology is more attractive at larger solids loads or where stabilization and energy recovery justify the investment. Smaller plants may need a simpler sludge treatment strategy.
Conclusion
Anaerobic sludge digestion provides more than sludge stabilization.
It can reduce biodegradable solids, control odors, produce biogas, and create an opportunity for energy recovery.
The process requires careful control of temperature, solids loading, retention time, mixing, and gas handling. Upstream sludge thickening and downstream dewatering should also be included in the design.
Mesophilic digestion remains a practical option for many wastewater applications. Thermophilic and multi-stage systems can provide additional process benefits when their higher complexity is justified.
Ultimately, the best anaerobic sludge digestion system is not simply the largest digester. It is a complete process designed around actual sludge characteristics, energy objectives, operating conditions, and final biosolids management.