How to select suitable storage equipment, calculate capacity, and manage sludge safely between treatment stages.
Introduction
Sludge production rarely matches transportation, disposal, or downstream processing schedules. Temporary storage helps wastewater treatment plants manage these differences.
A suitable storage arrangement also supports continuous operation during equipment maintenance, transport delays, and changing disposal schedules. Poor planning can cause overflow, odor complaints, difficult material handling, and unnecessary downtime.
The right solution depends on sludge consistency, solids concentration, storage duration, site conditions, and the next treatment step. Engineers should also consider mixing, drainage, ventilation, and environmental protection. The Ontario Sewage Works Design Guidelines discuss storage options for liquid, dewatered, and dried sludge. Their guidance provides a useful starting point, although local regulations must determine the final design.
Quick Reference: Sludge Storage
- Liquid sludge: Usually requires a tank, basin, or lagoon.
- Dewatered sludge cake: May use enclosed containers, bunkers, or covered storage areas.
- Dried biosolids: Often require bins, silos, or enclosed bulk storage.
- Capacity basis: Use measured sludge production and the required storage period.
- Volume calculation: Divide the required stored mass by the material’s bulk density.
- Mixing: Consider mixers or recirculation for liquid sludge that settles.
- Odor control: Assess ventilation, covers, extraction, and treatment requirements.
- Corrosion protection: Select materials according to sludge chemistry and site conditions.
- Transfer equipment: Match pumps, screws, or conveyors to sludge consistency.
- Safety: Assess confined spaces, hazardous gases, dust, access, and overflow risks.
1. What Is a Sludge Storage System?
A sludge storage system temporarily holds sludge before further treatment, transport, reuse, or disposal. It connects separate process stages and helps maintain stable plant operation.
Storage equipment varies according to the material’s physical state. Liquid sludge behaves differently from sticky dewatered cake or dry granules. Therefore, one storage arrangement rarely suits every application.
Common Applications
| Application | Typical material | Main purpose |
|---|---|---|
| Before dewatering | Thickened or liquid sludge | Balance feed fluctuations |
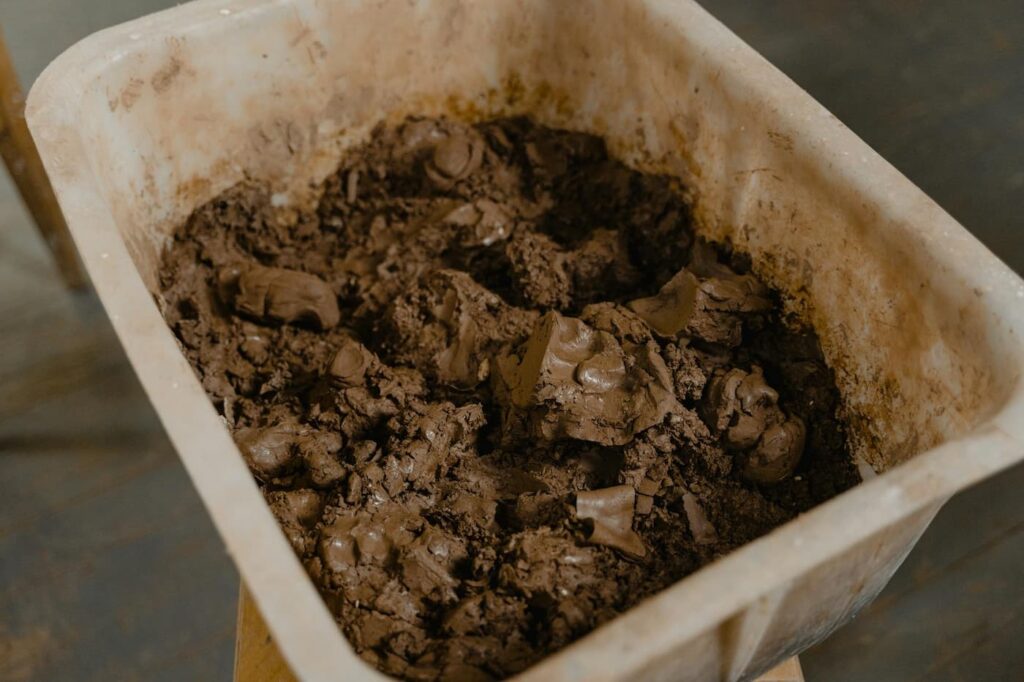
| After dewatering | Wet sludge cake | Buffer transport and disposal |
| Before drying | Dewatered sludge cake | Maintain a steady dryer feed |
| After drying | Dried sludge or biosolids | Hold material before shipment |
| During maintenance | Sludge from different process stages | Reduce disruption during downtime |
| Before beneficial reuse | Treated biosolids | Coordinate storage and collection |
A storage system may include more than a tank or silo. Pumps, mixers, level instruments, conveyors, ventilation, and drainage equipment can form part of the overall installation.
Typical Process Flow
Sludge thickening → Storage or equalization → Dewatering → Conveying → Drying or final storage → Transport or disposal
Actual process sequences vary. Some plants store sludge before dewatering, while others need only a short buffer after mechanical treatment.
2. Main Types of Sludge Storage Equipment
2.1 Sludge Storage Tanks

Sludge storage tanks commonly hold liquid or pumpable sludge. They may use concrete, coated carbon steel, stainless steel, or suitable polymer materials.
A tank can include a mixer, level sensor, drain connection, inspection opening, and sludge transfer pump. Covered designs can also support controlled ventilation and odor treatment.
Best suited for: Liquid sludge, pumpable mixtures, and intermediate storage before dewatering or further processing.
Key limitation: High-solids sludge may settle, bridge, or resist pumping. The tank and transfer equipment must match the actual material properties.
2.2 Sludge Holding Basins and Lagoons

Basins and lagoons provide storage over a larger footprint. Depending on the design, they may hold liquid sludge, partially thickened material, or other suitable sludge streams.
These systems can offer substantial capacity. However, they require careful consideration of liners, groundwater protection, rainfall, access, and sludge removal.
Best suited for: Sites with sufficient land and suitable environmental controls.
Key limitation: Open storage may create odor, runoff, and contamination risks. Longer retention can also change sludge properties.
2.3 Sludge Silos and Bulk Storage Bins

Silos and bins store dewatered or dried solids when the material can discharge reliably. Hopper bottoms help direct solids toward screws, conveyors, or other unloading equipment.
Their design must account for moisture, stickiness, bulk density, particle size, and discharge behavior. Wet sludge cake can adhere to walls and form stagnant zones.
Best suited for: Dried biosolids, suitable dewatered cake, and bulk solids that can flow through the outlet.
Key limitation: A silo designed for free-flowing granules may perform poorly with sticky cake. Material testing can help identify bridging and buildup risks.
2.4 Covered Sludge Storage Areas and Containers

Covered bunkers, enclosed bays, and containers provide temporary space for sludge cake or treated biosolids. They can simplify loading and collection when trucks operate on a scheduled basis.
The layout should provide enough room for loading machinery, cleaning, drainage, and safe personnel access. Roofs and covers also help prevent rainfall from rewetting stored material.
Best suited for: Dewatered sludge cake awaiting collection or further processing.
Key limitation: Open or poorly drained areas may generate contaminated runoff. Covered storage still needs appropriate ventilation and odor management.
2.5 Equipment That Supports Storage
Storage vessels work best when the surrounding equipment matches the sludge properties.
| Equipment | Function | Important selection factor |
|---|---|---|
| Mechanical mixer | Limits settling and improves uniformity | Viscosity, solids concentration, tank geometry |
| Recirculation pump | Moves sludge through a return loop | Flow rate, solids, abrasion, blockage risk |
| Sludge transfer pump | Moves pumpable sludge to another process | Rheology, solids, pipe length, elevation |
| Screw conveyor | Transfers sludge cake or suitable solids | Moisture, stickiness, distance, inclination |
| Level sensor | Monitors storage level | Foam, buildup, range, sensor compatibility |
| Ventilation system | Controls air movement in enclosed storage | Gas hazards, airflow, odor-treatment needs |
| Odor control unit | Treats extracted air | Airflow, odor load, treatment method |
| Drainage system | Collects liquid and washdown water | Contaminants, drainage rate, return route |
3. Comparison of Storage Options
The table below provides an initial screening guide. Final selection requires site-specific data.
| Storage type | Typical material | Main advantage | Main challenge |
|---|---|---|---|
| Storage tank | Liquid sludge | Enclosed and easy to integrate with pumps | Settling, corrosion, odor |
| Holding basin | Liquid or thickened sludge | Flexible capacity | Footprint and cleaning |
| Lagoon | Suitable liquid sludge | Large storage volume | Environmental controls and removal |
| Silo or bin | Dry solids or suitable cake | Compact bulk storage | Bridging and difficult discharge |
| Covered bunker | Dewatered cake | Flexible loading and collection | Space, drainage, odor |
| Container | Dewatered or dried solids | Convenient transport interface | Limited volume and handling frequency |
A tank generally fits pumpable sludge better than a dry bulk silo. A covered bunker may suit sticky cake that cannot discharge reliably through a hopper. For dried material, a silo may reduce the required footprint when discharge behavior has been verified.
4. How to Calculate Storage Capacity
Capacity should reflect sludge production, required storage duration, and the material’s physical properties. Avoid selecting a vessel from plant flow alone.
4.1 Estimate the Required Stored Mass
For a reasonably stable sludge production rate, calculate the required storage mass using this formula:
Required Stored Mass (kg) = Daily Sludge Production (kg/day) × Storage Duration (days)
Where:
- Required Stored Mass: Total sludge mass to be stored, in kg.
- Daily Sludge Production: Sludge generated per day, in kg/day.
- Storage Duration: Required storage period, in days.
This calculation assumes a relatively constant production rate. Actual designs should also account for downtime, seasonal variations, collection schedules, and emergency conditions.
4.2 Convert Mass to Storage Volume
For bulk solids, estimate the material volume using the following formula:
Material Volume (m³) = Required Stored Mass (kg) ÷ Bulk Density (kg/m³)
Where:
- Material Volume: Volume occupied by the sludge, in m³.
- Required Stored Mass: Total sludge mass, in kg.
- Bulk Density: Measured bulk density, in kg/m³.
For liquid sludge, engineers can estimate volume by dividing mass by density. When sludge concentration or composition varies, use measured density for a more reliable estimate.
4.3 Worked Example
Assume a plant produces 2,000 kg of dewatered sludge cake per day. The required buffer period is three days. Assume a measured bulk density of 800 kg/m³ for preliminary sizing.
| Parameter | Value |
|---|---|
| Daily sludge production | 2,000 kg/day |
| Storage duration | 3 days |
| Required sludge mass | 6,000 kg |
| Assumed bulk density | 800 kg/m³ |
| Calculated material volume | 7.5 m³ |
The calculated volume is 7.5 m³. This is the estimated volume occupied by the material, not the final vessel capacity.
Engineers must allow for unusable volume, operating limits, discharge geometry, and uncertainty in sludge production. The final design capacity will therefore exceed the calculated material volume where appropriate.
Engineering note
Do not apply one universal fill percentage to every sludge tank or silo. The usable volume depends on the vessel shape, level-control arrangement, mixing requirements, and discharge method.
5. Key Design Factors
5.1 Sludge Consistency and Solids Content
Moisture content strongly influences storage behavior. Liquid sludge may settle, while dewatered cake can stick to walls or compact under its own weight.
Dried biosolids may generate dust during filling and discharge. Engineers should confirm the material’s solids content, bulk density, flow behavior, and tendency to segregate.
5.2 Storage Duration
Short-term buffering and long-term storage have different design requirements. Longer retention may increase odor, settling, decomposition, or handling difficulties.
The U.S. EPA’s Guide to Field Storage of Biosolids discusses storage management and environmental concerns, including air quality, water quality, and sanitation. Its recommendations provide useful background, but project teams must follow applicable local rules and permits.
5.3 Mixing and Recirculation
Liquid sludge may separate during storage. A mixer or recirculation loop can improve uniformity and support reliable pumping.
However, excessive agitation may increase energy consumption or create unwanted foam. Engineers should assess mixer type, installation position, motor duty, and maintenance access.
5.4 Corrosion and Material Selection
Sludge chemistry determines the required construction materials and protective coatings. Chlorides, cleaning chemicals, temperature, and corrosive gases can affect equipment life.
| Component | Common considerations |
|---|---|
| Tank or basin | Structural loading, corrosion, chemical compatibility |
| Internal mixer | Immersion duty, seals, shaft and impeller material |
| Hopper and discharge | Abrasion, buildup, cleanout access |
| Pipes and valves | Solids passage, corrosion, blockage |
| Instruments | Moisture, foam, buildup, signal reliability |
| Covers and seals | Corrosion resistance and access requirements |
Carbon steel with a suitable protective system may suit some applications. Stainless steel, coated steel, concrete, or polymer construction may suit others. Verify compatibility against actual process conditions.
5.5 Odor, Ventilation, and Safety
Enclosed storage can help control odor, but it may also allow hazardous gases to accumulate. A risk assessment should cover ventilation, gas monitoring, access control, and confined-space procedures.
Dry sludge introduces a different concern: combustible dust may develop during handling. The design should assess dust extraction, ignition sources, and applicable explosion-protection requirements.
5.6 Site Layout and Maintenance Access
Storage equipment needs space for inspection, cleaning, and removal of accumulated solids. Truck routes and loading positions can also affect the required arrangement.
Designers should consider foundations, drainage, lifting equipment, electrical access, and emergency overflow protection. The storage location must also support safe operation during maintenance and abnormal conditions.
6. Storage Equipment Selection Matrix
Use this matrix for preliminary equipment screening. It does not replace detailed engineering.
| Sludge condition | Preferred starting option | Additional checks |
|---|---|---|
| Thin, pumpable sludge | Storage tank | Settling, mixer duty, pump compatibility |
| Thickened liquid sludge | Tank or holding basin | Viscosity, transfer pressure, retention |
| Sticky dewatered cake | Covered bunker or suitable container | Wall buildup, loader access, drainage |
| Cake feeding a dryer | Buffer hopper or bunker with feeder | Feed consistency, metering, bridging |
| Dried granular biosolids | Silo or bulk bin | Dust, discharge behavior, ventilation |
| Irregular collection schedule | Covered storage area or containers | Required buffer days, truck access |
| Corrosive industrial sludge | Chemically compatible storage equipment | Material testing, coatings, maintenance |
| Odor-sensitive location | Enclosed system with odor treatment | Airflow, capture, treatment capacity |
7. Integration with Dewatering and Conveying Equipment
Storage should match the equipment immediately before and after it. Otherwise, the system may create bottlenecks even when the vessel has sufficient volume.
Before Storage: Dewatering
Mechanical dewatering changes the sludge’s moisture content and physical behavior. A belt press, screw press, centrifuge, or filter press may produce cake with different handling characteristics.
See the related guide on sludge dewatering equipment for a comparison of common technologies. The actual moisture range depends on the feed sludge, conditioning, and machine configuration.
During Storage: Mixing and Level Control
Liquid sludge storage may require mixing, recirculation, or controlled withdrawal. Level instruments can support automatic pump operation and prevent overfilling.
The control strategy should reflect process needs. A simple high-level alarm may suit one installation, while another may require automatic feed interlocks and redundant instruments.
After Storage: Conveying and Feeding
Liquid sludge usually moves through compatible pumps and pipelines. Dewatered cake may need a screw conveyor, while suitable dried solids may use screws, belts, or other bulk-handling equipment.
Review the related sludge conveying equipment guide when selecting transfer equipment. Check the material’s behavior at startup, during continuous operation, and after an extended shutdown.
8. Illustrative Engineering Scenarios
The following scenarios are illustrative examples, not verified customer projects. They show how storage requirements can change across different applications.
Scenario A: Municipal Wastewater Plant
Region: Southeast Asia
Scale: Medium-sized municipal treatment facility
Challenge: Sludge collection schedules vary, and dewatering does not run continuously.
Design approach: Estimate daily cake production and the maximum likely collection delay. Consider a covered bunker with suitable loading access and drainage.
Expected engineering benefit: A correctly sized buffer can reduce disruption when transport is delayed.
Scenario B: Industrial Sludge Feeding a Dryer
Region: Central Europe
Scale: Industrial wastewater treatment line
Challenge: The dryer needs a stable feed, but upstream dewatering output fluctuates.
Design approach: Assess a buffer hopper or bunker with controlled discharge. Confirm that the feeder handles the actual cake consistency without bridging.
Expected engineering benefit: Better feed coordination can help reduce interruptions caused by uneven upstream production.
Scenario C: Dried Biosolids Awaiting Shipment
Region: North America
Scale: Regional sludge processing facility
Challenge: Dried material accumulates between production and scheduled transport.
Design approach: Evaluate a silo or covered bulk-storage area. Check dust control, ventilation, discharge reliability, and truck loading arrangements.
Expected engineering benefit: Suitable bulk storage can improve loading logistics and protect material from weather.
9. Maintenance and Troubleshooting
Routine inspection helps prevent storage failures and unplanned downtime. The maintenance schedule should follow the equipment manufacturer’s instructions and the site’s risk assessment.
| Problem | Possible cause | Recommended check |
|---|---|---|
| Sludge settles in the tank | Insufficient mixing or long retention | Review mixer operation and sludge properties |
| Cake sticks to the hopper | High moisture or unsuitable geometry | Inspect buildup and discharge surfaces |
| Silo outlet blocks | Bridging or compaction | Check outlet design and material flow behavior |
| Odor increases | Poor containment or inadequate air treatment | Inspect covers, extraction, and odor-control equipment |
| Corrosion appears | Incompatible materials or damaged coating | Assess chemical exposure and protective system |
| Level readings become unstable | Sensor fouling, foam, or poor placement | Clean and verify the sensor |
| Storage overflows | Inadequate capacity or control failure | Check production assumptions, alarms, and interlocks |
| Drainage water accumulates | Blocked drain or poor floor design | Inspect drainage and the return route |
Inspection work must follow appropriate isolation and confined-space procedures. Personnel should not enter a tank or silo without the required permits, testing, and protective measures.
10. Information Required for a Storage Equipment Quotation
A useful request for quotation should describe the sludge, the operating schedule, and the required interfaces. This helps suppliers avoid sizing equipment from incomplete assumptions.
| Information | Details to provide |
|---|---|
| Sludge source | Municipal, industrial, biological, chemical, or mixed |
| Physical condition | Liquid, thickened, dewatered cake, or dried solids |
| Solids content | Measured dry-solids percentage |
| Daily production | kg/day, tonnes/day, or m³/day |
| Bulk density | Required for preliminary bulk-solids volume calculations |
| Storage duration | Normal and maximum expected holding period |
| Required capacity | Working volume or required buffer mass |
| Site conditions | Indoor or outdoor, temperature, corrosion exposure |
| Transfer method | Pump, screw conveyor, belt conveyor, loader, or truck |
| Mixing requirements | Continuous, intermittent, or no mixing |
| Odor and ventilation | Enclosure, air extraction, and treatment requirements |
| Instrumentation | Level sensors, alarms, interlocks, and control signals |
| Materials | Required construction materials or chemical compatibility |
| Layout | Dimensions, elevations, access, and connection points |
| Applicable standards | Local environmental, structural, electrical, and safety requirements |
Where sludge properties vary, provide representative samples or laboratory data. Photographs and process flow diagrams can also help suppliers understand access limitations and transfer interfaces.
11. Common Sludge Storage Design Mistakes
- Sizing from average production only: Maximum production and collection delays can create larger storage demands.
- Ignoring sludge properties: Sticky cake and free-flowing granules need different discharge arrangements.
- Selecting a tank without checking settling: Poor mixing can cause uneven solids concentration and difficult removal.
- Overlooking odor control: Covers alone do not guarantee effective odor management.
- Forgetting drainage: Wash water and contaminated runoff need a defined collection route.
- Using unsuitable materials: Corrosion can damage the vessel, piping, or internal components.
- Ignoring downstream equipment: A large storage vessel cannot compensate for an undersized feeder or conveyor.
- Treating all dried sludge as safe bulk material: Dust and gas hazards require a project-specific assessment.
12. Engineering Recommendation
Choose storage equipment based on the material’s condition, required buffer period, and downstream process. Do not select a vessel by capacity alone.
For liquid sludge, prioritize transfer reliability, mixing needs, and odor control. For sticky cake, examine discharge geometry and access for cleaning. For dried biosolids, assess bulk flow, dust control, ventilation, and unloading arrangements.
The most reliable design combines suitable storage capacity with compatible pumps, feeders, instrumentation, and maintenance access. A complete process review is more useful than evaluating the storage vessel in isolation.
13. Frequently Asked Questions
Storage Types and Capacity
What is the main purpose of sludge storage equipment?
It provides temporary capacity between treatment, transport, and disposal stages. Storage can help manage production fluctuations, maintenance periods, and collection delays.
How do I calculate the required storage volume?
Estimate the sludge mass produced during the required holding period. Divide that mass by the measured density or bulk density, then account for usable capacity and operating requirements.
Can dewatered sludge be stored in a silo?
Yes, when the material can discharge reliably through the silo outlet. Sticky or highly cohesive cake may require a bunker or another arrangement instead.
Operation and Equipment Selection
Does every sludge storage tank need a mixer?
No. The need depends on solids concentration, settling behavior, storage duration, and process requirements. Some installations can operate without continuous mixing.
What information should I provide when requesting a quotation?
Provide sludge type, solids content, production rate, storage duration, required capacity, transfer method, site layout, and applicable standards. Include odor-control and instrumentation requirements where relevant.
Conclusion
Well-designed storage connects sludge treatment stages and helps maintain reliable plant operation. The right solution depends on sludge consistency, capacity requirements, storage duration, and environmental controls.
For a suitable equipment selection, evaluate the entire storage and transfer arrangement. Confirm the design basis before finalizing the vessel, mixer, feeder, and control system.
Planning a Sludge Storage System?
Share your sludge characteristics, daily production, storage duration, and site layout with the Morvolous team. We can help review the equipment configuration and key selection requirements for your application.
Author
Morvolous Engineering Team
Morvolous provides wastewater treatment equipment and process-oriented guidance for industrial and municipal applications. Our technical content focuses on equipment selection, system integration, and practical engineering considerations.